Waste Tire Recycling System
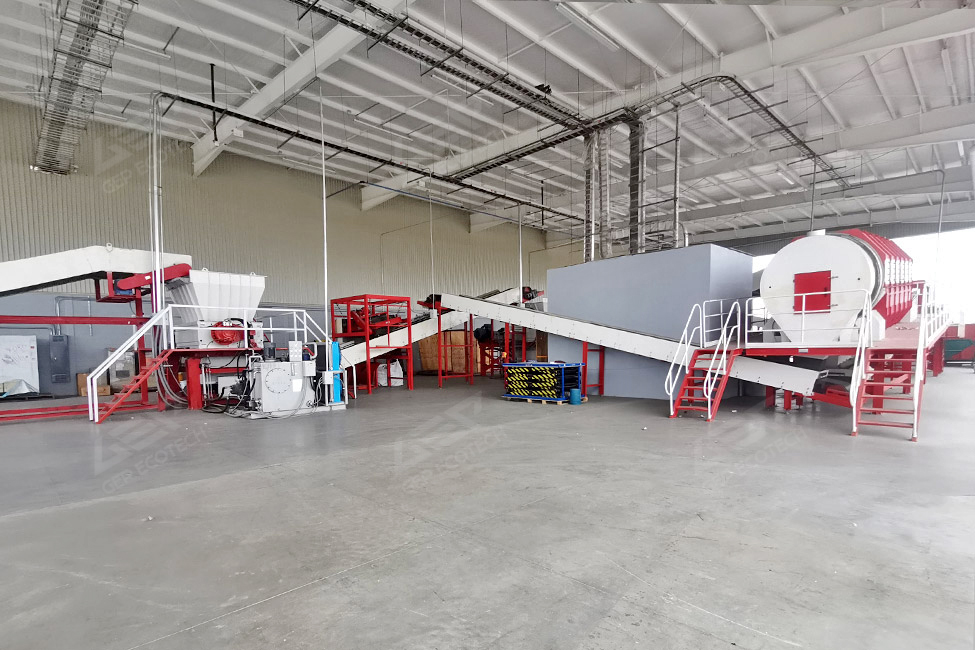
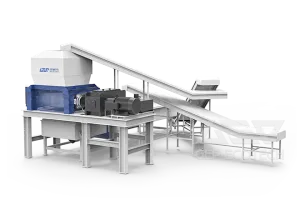
- Integrated shredding and screening with cost-effective layout.
- Produces clean, high-calorific rubber chips for direct coal substitution.
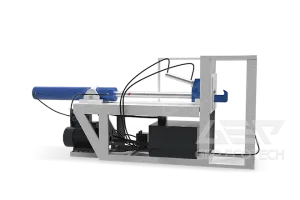
- Optional debeader removes steel wires, protecting back-end equipment.
- Adaptable modules handle varied feeds, meeting output requirements.
- Smart monitoring enables automated production, minimal manual input.
- Durable components minimize downtime, ensuring consistent output.
- Automated controls and easy maintenance lower intervention, energy, costs.
- Modular units adjust to tire type, capacity, mesh sizes.
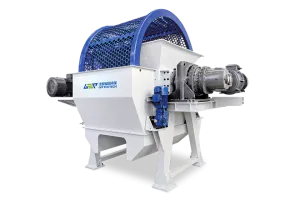
- Optional fiber separator removes textiles, improving final powder purity.
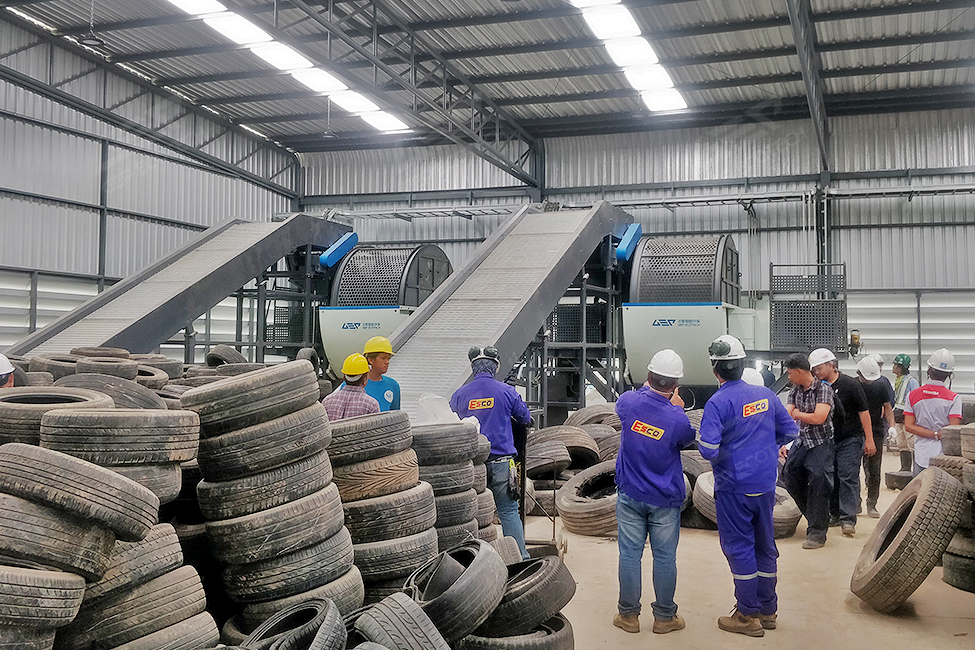
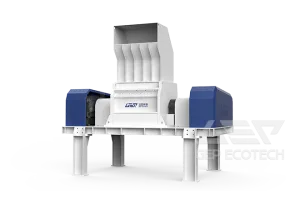
- Integrated shredding-grinding layout ensures smooth, efficient production.
- Integrated modules enable excellent rubber, steel, fiber recovery.
- Smart control ensures coordinated operation, monitoring, fault alerts.
- Separators remove bead, textiles, ensuring clean rubber feedstock.
- Modular design adapts to tire types, particle sizes.
- Produces uniform, clean rubber powder for continuous pyrolysis.
C&D Waste Recycling System
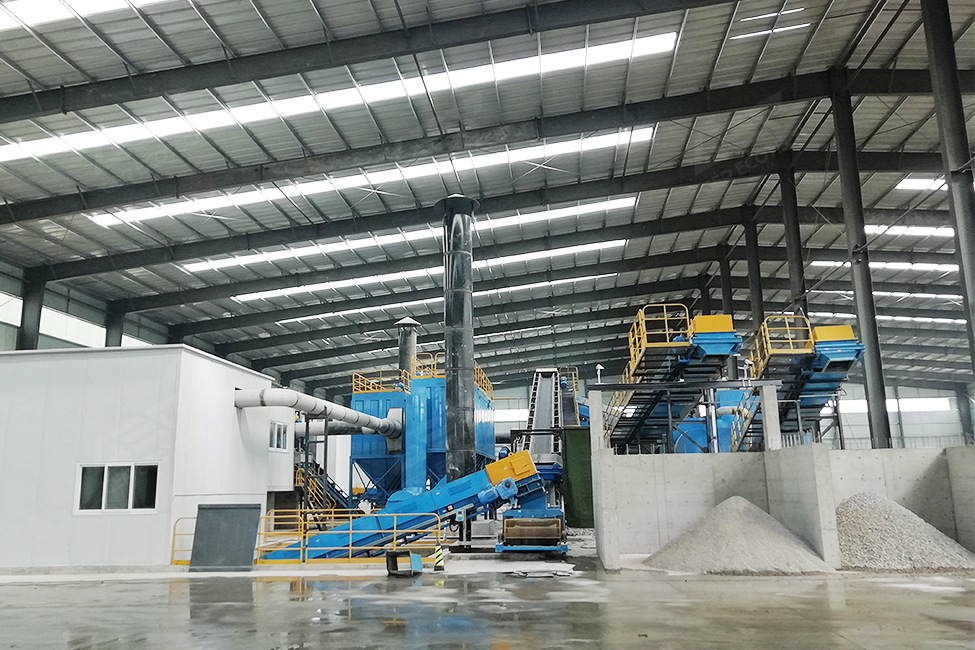
- Crushing and sorting solution produces high-purity recycled aggregates.
- Integrated system ensures stable, continuous, efficient operation.
- Modular screening, wind sifting ensure consistent output quality.
- Precise separation recovers metals, turning waste into revenue.
- Multi-stage sorting ensures high-purity output, reduces crusher wear.
- Sorting-first pre-removes impurities, reducing crushing volume, difficulty.
- Streamlined flow ensures stable operation, high recovery.
- Waste becomes marketable aggregates, cutting costs, earning revenue.
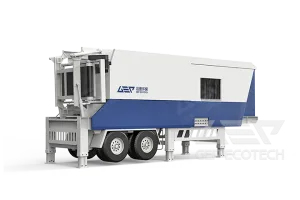
- Enables quick transport, on-site setup, immediate source operation.
- Eliminates long-distance transport, landfill fees via on-site processing.
- Modular plug-and-play design configures easily for diverse projects.
- No permanent foundations; high resale value, easy relocation.
- Dust suppression, optional washing ensure local environmental compliance.
Core Equipment
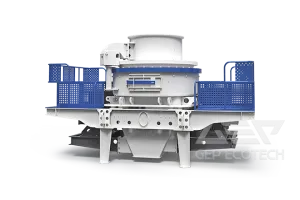
MSW Recycling System
- Produces uniform and high-calorific RDF pellets for coal substitution.
- Flexible layout handles varied waste, calorific and moisture contents.
- Automated process reduces manual input, ensuring efficient operation.
- Dust control prevents pollution; sorting removes hazardous materials.
- Robust, energy-efficient equipment and remote monitoring cut downtime.
- Simplified system cuts capital, energy costs for landfill projects.
- Screening, air, magnetic sorting separate stale waste fractions.
- Trommel, wind sifter, magnets speed separation and cut handling.
- Reliable equipment ensures stable and low-maintenance operation.
- Recovers metals, fuel bales, and cover soil; cuts landfill volume.
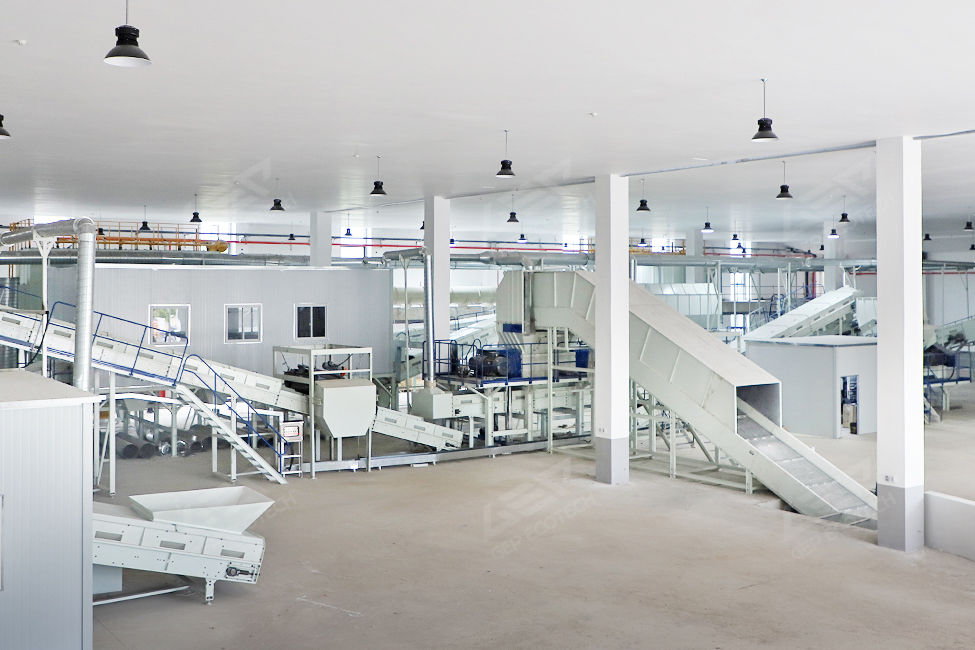
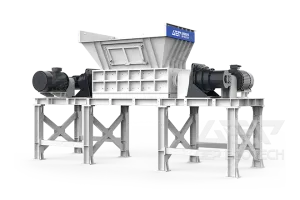
RDF&SRF Production System
- Two-stage shredding, multi-stage sorting ensure high-calorific fuel.
- PLC control enables automated, safe, near-unattended production.
- Modular design adapts to feedstock and product requirements.
- Integrated layout ensures smooth, closed, low-dust material flow.
- Shredding, screening, air classification ensure high-calorific, stable RDF/SRF.
- Centralized PLC control enables stable, near-unattended operation.
- Modular flow handles MSW fluctuations, ensuring consistent fuel.
- Streamlined layout cuts transfer distance, fuel production costs.
- Multi-stage sorting isolates light combustibles for high-calorific RDF/SRF.
- Heavy-duty shredders, wear-resistant parts withstand demolition waste.
- Recovers metals, converts combustibles to fuel, diverts landfill.
- Shredding, sorting, densification ensure efficient, compact flow.
- Dual-shaft shredder, hammer mill ensure uniform particles.
- High pressure produces durable, high-density, high-calorific pellets.
- Magnetic, air separation produce clean renewable fuel.
- Automated control ensures stable and efficient continuous production.
Hazardous Waste Recycling System
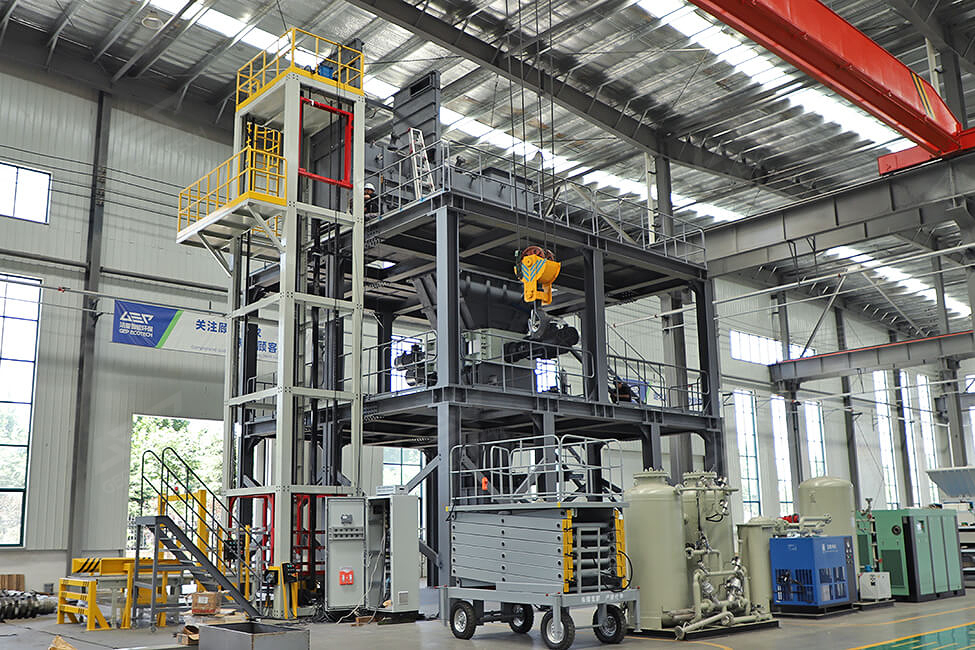
- Sealed N₂ environment, automatic fire suppression prevents combustion.
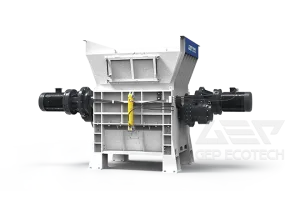
- Flexible configuration, suitable for primary, medium, fine shredding.
- PLC monitoring, O₂ control, interlocked subsystems enable automation.
- Tower design consolidates processes into small, efficient footprint.
- Retractable cutter box allows quick access, reducing downtime.
Biomass Recycling System
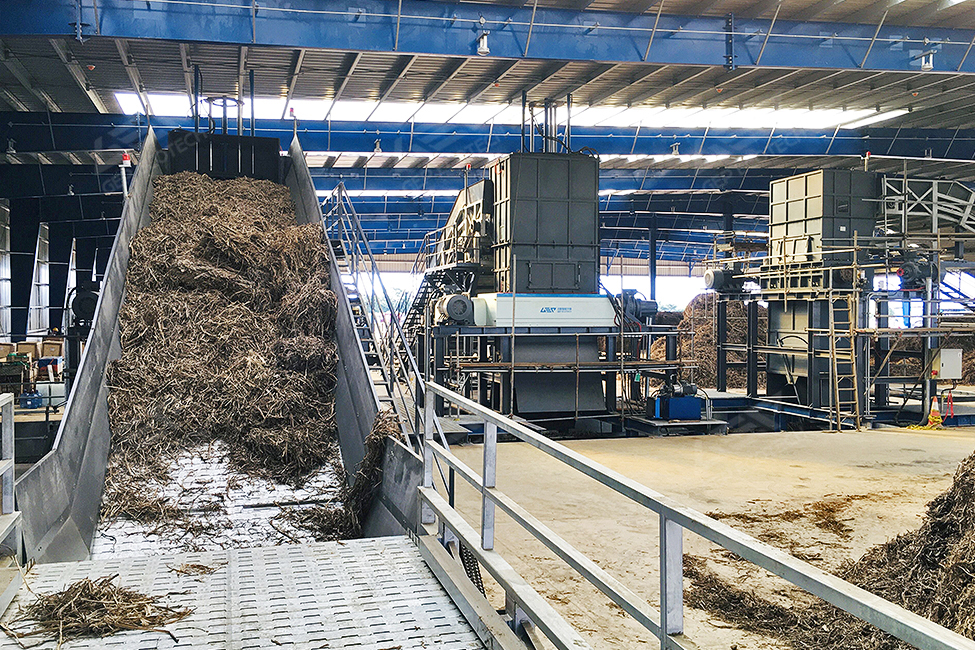
- Heavy-duty chain conveyor prevents clogging, ensuring steady supply.
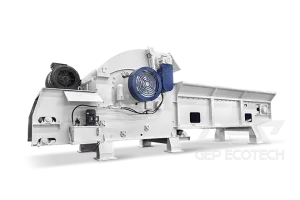
- Double-shaft shredder ensures stable, high-volume primary shredding.
- Integrated system enables real-time monitoring, for easy maintenance.
- Magnetic separator removes ferrous metals, improving fuel quality.
- Pulse dust collector controls particles, ensuring compliant workspace.
- Intelligent conveyors prevent clogging, ensuring continuous downstream.
- Multi-stage shredding and screening ensure uniform particles.
- Magnetic separator removes ferrous metals, boosting purity.
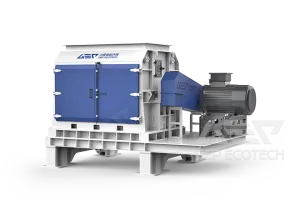
- Hammer mills finely grind biomass below 10 mm.
- Combines heavy-duty and fine shredding for uniform particles.
- Magnetic and air separation ensure clean, high-quality fuel.
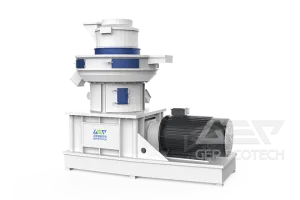
- Compresses material into dense, high-calorific, transportable pellet fuel.
- Central monitoring enables real-time control and predictive maintenance.
Core Equipment
C&I Waste Recycling System
- Stepwise shredding ensures uniform particle size for high-quality RDF.
- Magnetic and air separation remove impurities, raising fuel calorific value.
- Centralized automated control ensures safe and efficient operation.
- Configurable to produce dense RDF pellets or compact bales.
- Built-in pulse dust collector controls dust, ensuring cleaner production.
- Three-stage shredding ensures uniform size reduction for high-quality SRF.
- Post-secondary magnetic separation maximizes ferrous metal purity.
- Specially engineered cutters reduce replacements, and maintenance costs.
- Lower energy consumption significantly reduces operational expenses.
- Hydraulic baler produces dense, uniform SRF bales for easy handling.
- The shredder combination ensures uniform output for high-quality fuel.
- Magnetic-air separation removes impurities, raising fuel calorific value.
- Smart control ensures efficient production reducing labor cost.
- Configurable to produce dense RDF pellets and compact SRF bales.
- Dust collection controls pollution, ensuring environmental compliance.